Green hydrogen production involves splitting water into hydrogen and oxygen through electrolysis powered by renewable electricity from sources such as solar and wind. Its green credentials depend on the electricity source, not electrolysis alone. The process requires more than an electrolyzer, integrating treated water, renewable power, gas separation, hydrogen purification and supporting equipment to achieve the required purity, pressure and production rate.
Green hydrogen can help reduce production-related emissions, decarbonize hard-to-abate industries and convert surplus renewable electricity into a storable energy carrier. However, its environmental and economic benefits depend on renewable power availability, water supply, equipment efficiency and the engineering of the complete production system.
This article aims to explain how green hydrogen is produced, compares the principal electrolysis technologies, examines the production process step by step, and explores the engineering considerations involved in developing an industrial-scale green hydrogen facility.
How Is Green Hydrogen Produced?
Green hydrogen is produced by using renewable electricity to split water into hydrogen and oxygen in an electrolyzer. The overall chemical reaction is:
2H2O → 2H2+O2
The two primary inputs are water and electrical power. The electrolyzer uses electrical energy to drive the reaction, producing hydrogen at one electrode and oxygen at the other. The resulting hydrogen is then processed to meet the purity and moisture specifications required by its intended application. The US Department of Energy explains the underlying process in its guide to hydrogen production through electrolysis.
What Distinguishes Green Hydrogen From Other Types?
| Hydrogen type | Production method | Key characteristic |
| Grey hydrogen | Fossil fuels, typically natural gas, without carbon capture | Associated with substantial production-related emissions |
| Blue hydrogen | Fossil-fuel-based production with carbon capture | Emissions depend on capture performance and upstream emissions |
| Green hydrogen | Water electrolysis powered by renewable electricity | Environmental performance depends on the electricity and wider supply chain |
| Low-carbon hydrogen | Production pathways meeting applicable emissions-intensity criteria | A broader category whose definition varies by jurisdiction |
These classifications are common industry conventions. Certification schemes and regulations may use different emissions thresholds and accounting boundaries.
Green Hydrogen Production Process: Step by Step
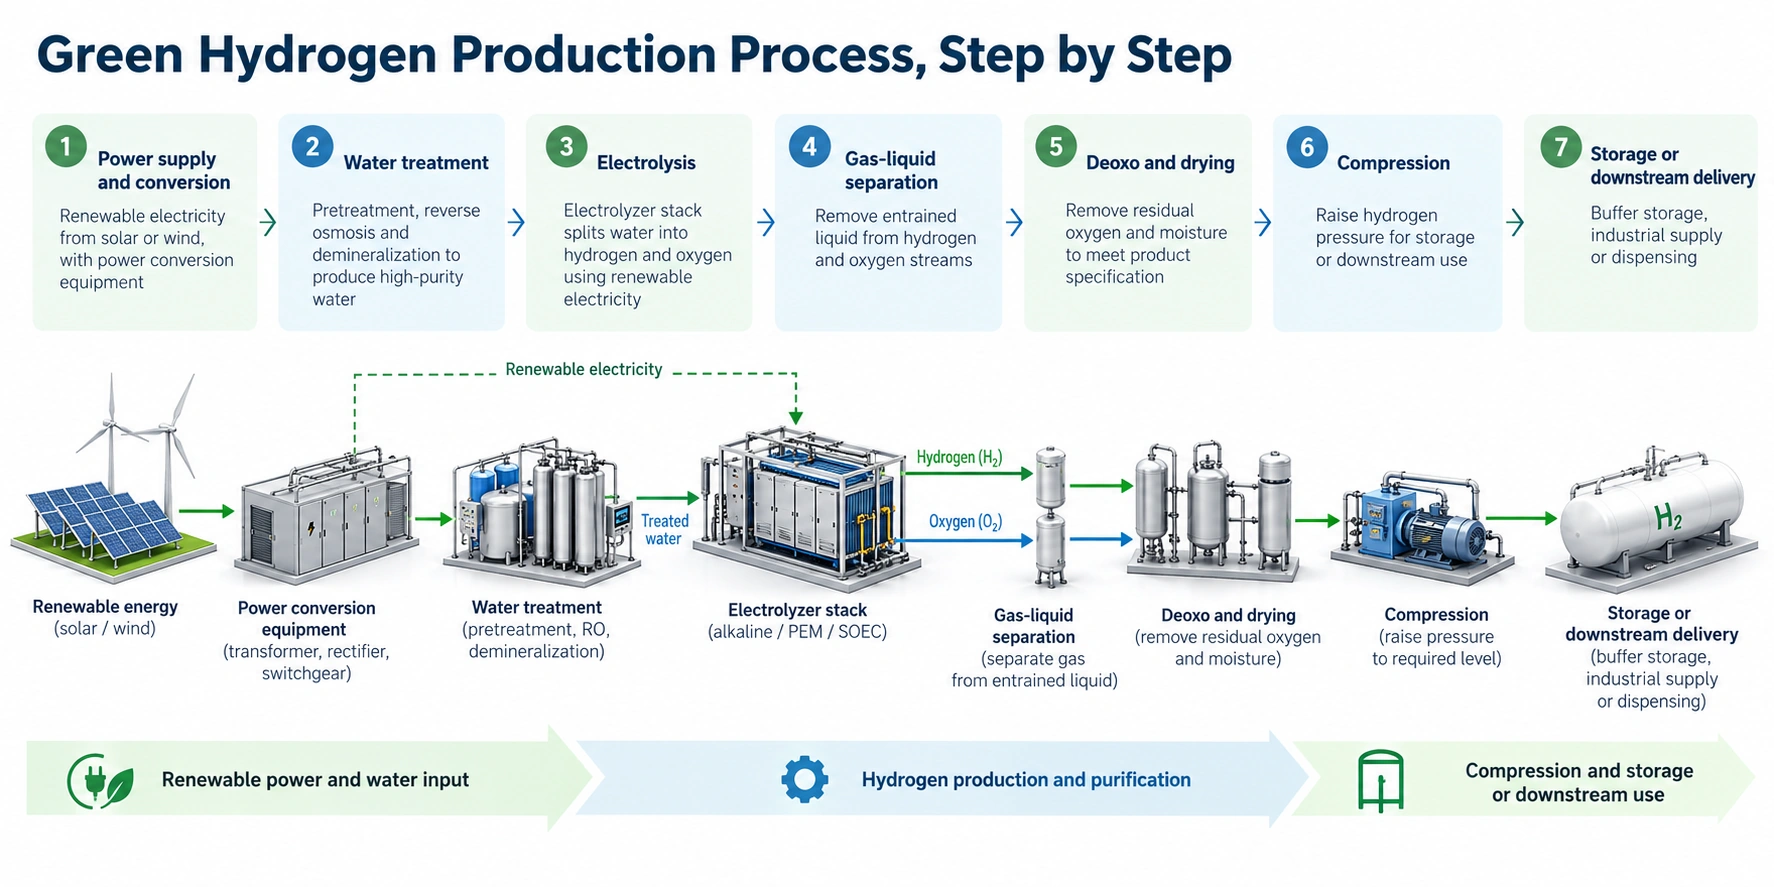
The green hydrogen production process combines water electrolysis with supporting systems that condition the feedwater, manage the gases and prepare the hydrogen for downstream use. Understanding each stage helps explain the complete process of green hydrogen production and the interfaces that must be coordinated during plant engineering. The process flow provides the starting point for equipment sizing, utilities design, safety reviews and coordinated multidisciplinary engineering at industrial scale.
Step 1: Power supply and conversion
Renewable electricity from a solar or wind installation supplies the electrolyzer system. Depending on the configuration, transformers, switchgear, rectifiers or power-conversion units regulate the electrical supply to meet the electrolyzer’s voltage, current and operating requirements. Power-system design must also consider protection, power quality, operating flexibility and the availability of renewable generation.
Step 2: Water treatment
Water is treated to meet the electrolyzer manufacturer’s feedwater quality requirements. A typical treatment train may include pretreatment filters, activate carbon where required, reverse osmosis, demineralization or electrodeionization, and a treated-water tank. The precise arrangement depends on raw-water quality, the electrolyzer technology and vendor specifications. Water quality is essential to protect the stack and maintain reliable operation.
Step 3: Electrolysis
The electrolyzer stack is the central hydrogen-generation component. It contains electrochemical cells that use electrical energy to split water into hydrogen and oxygen. Alkaline electrolysis is a mature commercial option, while proton exchange membrane (PEM) electrolysis is another established technology. Solid oxide electrolysis cells (SOEC) operate at high temperatures and can benefit from integrated heat sources. Technology selection affects the electrical system, water requirements, operating flexibility and plant interfaces.
Step 4: Gas-liquid separation
The gas streams leaving the electrolyzer may contain entrained liquid and require separation before further processing. Gas-liquid separators, sometimes integrated with electrolyte circulation and cooling equipment, separate the gas from liquid water or electrolyte. The hydrogen and oxygen streams are handled independently, with appropriate controls and safeguards to prevent unsafe gas mixing.
Step 5: Deoxo and drying
Hydrogen may require further purification to meet the required product specification. Where residual oxygen must be removed, a deoxo unit uses a catalytic reaction to convert oxygen and hydrogen into water. A downstream dryer, such as a desiccant-based drying system, removes moisture to achieve the required dew point. The actual purification train depends on the electrolyzer outlet quality and the end-use specification.
Step 6: Compression
A hydrogen compressor raises the gas pressure to suit the downstream process, storage system or dispensing application. Compressor selection considers inlet and discharge pressure, flow rate, gas temperature, materials compatibility, sealing arrangements, cooling and operating profile. Compression requirements vary by application, so the final configuration should be determined from the process design basis.
Step 7: Storage
Hydrogen is routed to appropriately designed storage vessels or buffer systems when required by the operating concept. Storage capacity, pressure rating, layout, isolation, ventilation, gas detection and emergency provisions must be assessed as part of the plant design.
For a broader view of the downstream stages, readers can explore Rishabh Pro Engineering’s Green Hydrogen Value Chain . The process flow provides the starting point for equipment sizing, utilities design, safety reviews and coordinated multidisciplinary engineering at industrial scale.
The seven stages outlined above illustrate how renewable electricity and treated water are converted into hydrogen and conditioned for downstream use. However, the equipment configuration, operating conditions and energy requirements can vary depending on the electrolyzer technology selected. Understanding these differences is essential when evaluating plant efficiency, operational flexibility and balance-of-plant requirements.
The following section examine the key method used to translate this process flow into an integrated design, from defining equipment and utility requirements to coordinating interfaces and validating the overall system.
Green Hydrogen Production Methods Compared
The choice of electrolysis technology affects electricity consumption, equipment arrangement, operating flexibility, maintenance requirements and overall plant economics. Alkaline and PEM systems are commercially established, while SOEC and AEM have different levels of commercial maturity and technical readiness.
The following comparison draws on IRENA’s Green Hydrogen Cost Reduction report from 2020. Temperature ranges are indicative and vary by manufacturer.
| Parameter | Alkaline (AWE) | PEM | SOEC | AEM |
| Typical operating temperature | 70–90°C | 50–80°C | 700–850°C | 40–60°C |
| Commercial maturity | Established commercial technology | Established commercial technology | Demonstration and early commercialization vary by system | Emerging technology |
| Main strength | Mature technology and established supply chain | Compact system and rapid response to changing loads | Can use heat or steam to reduce electrical energy requirements | Potential to combine membrane-based operation with less reliance on precious-metal catalysts |
| Main limitation | Liquid electrolyte management and operating flexibility considerations | Membrane durability and reliance on certain costly catalyst materials | High-temperature materials, thermal cycling and durability | Membrane stability, durability and long-term commercial validation |
| Key engineering consideration | Electrolyte circulation, separation and maintenance | Water quality, power conversion and gas management | Thermal integration, insulation and heat management | Membrane performance, electrolyte management and technology-specific vendor requirements |
The table is a general technology overview, not a performance guarantee. Actual efficiency, pressure, operating limits, lifetime and maintenance intervals must be established from the selected OEM’s technical documentation.
Other Renewable Hydrogen Production Pathways
Beyond conventional electrolysis, researchers are developing several alternative hydrogen production pathways. Biomass gasification converts organic material into a hydrogen-containing synthesis gas that can be processed and purified. Its emissions profile depends on feedstock sourcing, process energy, conversion efficiency and emissions management.
Photoelectrochemical (PEC) water splitting uses light-absorbing semiconductor materials to drive water splitting directly. Photobiological production investigates biological processes through which microorganisms can generate hydrogen. Solar thermochemical water splitting uses concentrated solar heat to drive chemical reactions that release hydrogen.
These approaches offer different possibilities for renewable hydrogen generation, but their technical maturity, efficiency, durability and commercial readiness vary. Most are not yet interchangeable with established commercial electrolyzer systems for conventional industrial projects. The US Department of Energy’s hydrogen production overview provides further information on these research pathways.
How to Generate Green Hydrogen at Industrial Scale
Industrial-scale green hydrogen generation requires the coordinated design of the electrolyzer, balance of plant (BoP), utilities, electrical systems, safety provisions and downstream interfaces. The electrolyzer is central to the facility, but the complete plant determines the usable output and operating performance.
- Establish the design basis: Define the required hydrogen production rate, purity, delivery pressure, operating hours, availability and downstream application. Assess renewable power availability, water quality, site conditions and the expected operating profile before selecting the electrolyzer technology.
- Select and size the electrolyzer: Compare alkaline, PEM and other suitable technologies against capacity, operating flexibility, efficiency, maintenance, vendor support and lifecycle requirements. Evaluate the complete system’s power demand, including auxiliary equipment, rather than relying only on the stack’s rated performance.
- Engineer the balance of plant: Develop process flow diagrams (PFDs), piping and instrumentation diagrams (P&IDs), heat and mass balances, equipment datasheets and utility summaries. The BoP may include water treatment, gas-liquid separation, cooling, purification, electrical conversion, instrumentation and control systems.
- Integrate renewable power and utilities: Coordinate renewable electricity with electrical distribution, protection, cooling, ventilation and other site utilities. The operating strategy must account for changing power availability and the electrolyzer’s permitted operating range. Power management, buffering or other measures may help address variability, subject to technical and economic assessment.
- Plan modularization and plant layout: Skid-mounted or containerized packages can standardize equipment assemblies and simplify fabrication and site installation. However, modularization requires early coordination of transport dimensions, lifting provisions, maintenance access, piping, electrical connections and package interfaces.
- Integrate safety and controls: Hydrogen systems require careful consideration of leakage, ventilation, ignition sources, pressure protection, material compatibility and emergency isolation. Hazard identification, HAZOP, hazardous-area classification, gas detection and emergency response provisions should be integrated into the design process.
- Validate the integrated design: Multidisciplinary reviews should evaluate equipment interfaces, operating scenarios, maintainability and constructability. Process, piping, mechanical, civil and structural, electrical, and instrumentation and control teams must work from a coordinated design basis to minimize interface gaps and late-stage revisions.
Challenges in Green Hydrogen Production
The production of green hydrogen faces challenges involving energy consumption, production cost, renewable power variability and water availability.
- Cost: Green hydrogen production remains more expensive than fossil-based hydrogen. BloombergNEF estimated production costs of approximately US$4–12/kg in 2024, depending on project conditions. Renewable electricity prices and electrolyzer capital costs are key drivers.
- Infrastructure, Storage and Transportation: Developing hydrogen production, storage and distribution infrastructure requires substantial investment and coordination across the supply chain. Hydrogen’s low volumetric energy density also necessitates specialized storage and transportation systems, increasing costs and engineering complexity.
- Energy Consumption: Electrolyzer efficiency affects operating costs. IRENA reports indicative electricity consumption of 50–78 kWh/kg for alkaline, 50–83 kWh/kg for PEM and 45–55 kWh/kg for SOEC electrolysis. Scaling up also requires reliable renewable power and adequate water supplies.
- Power variability and Water supply: Renewable power variability can reduce electrolyzer utilization. Batteries and flexible operation may help manage fluctuations, while direct electrification may be more cost-effective for some applications. Water availability and treatment requirements also influence project feasibility.
How Rishabh Pro Engineering Supports Green Hydrogen Production
Green hydrogen production facilities require coordinated engineering across process systems, equipment, utilities, electrical infrastructure, piping, structures and instrumentation. We, as green hydrogen engineering consultants support this integration through multidisciplinary design engineering, with a focus on equipment interfaces, safety, maintainability, modularization and constructability.
Our engineering scope can include:
- End-to-end engineering support: From FEED (Front-End Engineering Design) to detailed engineering, we cover all aspects—mechanical, piping, civil & structural, electrical, and instrumentation.
- Process engineering: Process flow diagrams, P&IDs, heat and mass balances, equipment sizing and HAZOP support.
- Equipment and piping engineering: Equipment datasheets, piping specifications, 3D CAD modeling, pipe stress analysis and package interfaces.
- Structural engineering: Equipment supports, skid structures, foundations and container arrangements.
- Electrical engineering: Power distribution, electrical load lists, single-line diagrams and cable sizing.
- Instrumentation and control engineering: Instrument indexes, I/O lists, control philosophy and technology-package integration.
- Balance-of-plant engineering: Integration of water treatment, cooling, gas handling, purification and auxiliary systems.
- Modularization and layout engineering: Equipment arrangements, maintenance access, interface management and fabrication-oriented design.
- Procurement and vendor support: Technical documentation, equipment specifications and vendor document coordination.
Case Study: 200 Nm³/hr Green Hydrogen Production and HRS Facility – Multidisciplinary Engineering
Project overview:
Rishabh Pro Engineering supported the development of a 1 MW green hydrogen production facility in Gujarat, India, integrated with a Hydrogen Refueling Station (HRS). The facility uses alkaline water electrolysis, with a stated production capacity of 200 Nm³/hr and captive solar power. The project was designed around a 25-year commercial operating life.
The facility integrates hydrogen generation with downstream processing, high-pressure storage and vehicle refueling infrastructure.
Key engineering scope:
- Multidisciplinary balance-of-plant engineering and electrolyzer package integration.
- Process documentation, utility planning and equipment datasheets.
- Plant layout, 3D modelling, piping design and equipment coordination.
- Mechanical equipment, buffer storage and hydrogen compression interfaces.
- Electrical distribution, instrumentation, controls and technology-package integration.
- Civil and structural engineering, fire protection and process safety coordination.
- Integration considerations for H35 and H70 dispensing, with high-pressure cascade storage.
Engineering focus:
The project required coordination between the electrolyzer technology package, supporting utilities, high-pressure hydrogen systems and refueling interfaces. The engineering approach focused on integrating these systems into a coordinated facility design while addressing safety, maintainability and package interfaces.
Concluding Thoughts
Green hydrogen production is not simply an electrolyzer selection exercise. The performance of an industrial facility depends on the integration of renewable power, water treatment, electrolysis, gas purification, utilities and downstream delivery systems.
Selecting the appropriate electrolysis technology is only the starting point. Engineering teams must also evaluate energy consumption, operating flexibility, equipment interfaces, safety, maintainability and the practical constraints of the site.
Rishabh Pro Engineering supports green hydrogen projects through process and balance-of-plant engineering, multidisciplinary design, equipment integration and modularization. A system-led engineering approach helps project teams address interface risks early and develop facilities that align with their production and operating requirements.
Frequently Asked Questions On Green Hydrogen Production
Q: What is green hydrogen production?
A: Green hydrogen production is the generation of hydrogen using renewable energy, commonly by splitting water into hydrogen and oxygen through electrolysis. Its environmental performance depends on the electricity source and the wider production lifecycle.
Q: Which electrolyzer technology is best for industrial-scale green hydrogen production?
A: There is no universally best technology. Alkaline electrolysis is a mature commercial option, PEM can suit applications requiring rapid response to variable power, SOEC may benefit from integrated high-temperature heat, and AEM remains an emerging technology. Selection depends on project capacity, operating profile, efficiency, cost and lifecycle requirements.
Q: What equipment is required for a green hydrogen production plant?
A: A typical plant includes power-conversion equipment, water-treatment systems, an electrolyzer stack, gas-liquid separators, purification and drying equipment, and supporting cooling, instrumentation and control systems. Compressors and storage vessels are included when required by the delivery and operating concept.
Q: How much electricity is required to produce 1 kg of green hydrogen?
A: Electricity consumption depends on the electrolyzer technology, operating conditions and system configuration. Indicative technology-level estimates range from approximately 50–83 kWh per kg of hydrogen for alkaline and PEM electrolysis, while high-temperature SOEC systems may require less electrical input when integrated with a suitable heat source. Actual plant consumption also depends on auxiliary equipment and balance-of-plant requirements.
Q: What role does water treatment play in green hydrogen production?
A: Water treatment ensures that feedwater meets the electrolyzer manufacturer’s quality requirements. Processes such as reverse osmosis and demineralization help remove impurities that could affect electrolyzer performance, equipment life and operational reliability. The treatment configuration depends on the raw-water source and the selected electrolysis technology.
Q: What factors influence the cost of green hydrogen production?
A: Key cost drivers include renewable electricity prices, electrolyzer capital costs, energy consumption, plant utilization, maintenance and balance-of-plant requirements. Variability in solar and wind power can affect operating hours, while water availability and treatment, compression and storage requirements add to overall project costs. Efficient plant integration and appropriate technology selection can help improve project economics.